Alright, let’s cut to the chase—if you’re deep in the machining game, you’ve probably stared at a wall of machine tools and wondered: vertical vs horizontal machining centers (VMCs vs HMCs) which one’s actually worth your hard-earned cash? I’m Jake, been selling VMCs for over 12 years, so I’ve fielded this question a thousand times from small shop owners to big aerospace guys. Most folks I talk to mix up the basics at first, but the difference boils down to one super simple thing: the orientation of the spindle. Wait, no, hold up—don’t zone out yet, because that tiny spin axis changes literally everything about how your parts get made. Vertical Machining Center
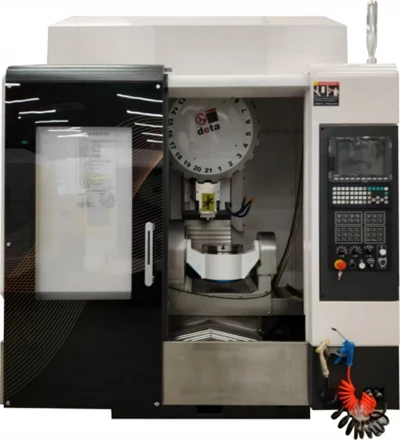
Let’s start with the easy one: vertical machining centers, aka VMCs. The spindle sticks straight down toward the work table, right? Like a drill press but way smarter. When I sell a VMC, I always point out the biggest win first: it’s user-friendly. No fancy setup required. Stick a part on the table, clamp it, load the program, and you’re off. That’s why 70% of small to mid-sized shops run at least one VMC—they’re perfect for quick prototypes, one-off custom parts, or small batch jobs. Last quarter, I sold a 3-axis VMC to a guy who makes custom fishing rod reels; he needed to mill aluminum handles fast, no extra steps. VMCs handle that like a dream, no overcomplicating things.
Now, the horizontal machining center, HMC, the bad boy of the group. Its spindle spins side to side, parallel to the floor, not straight down. That tiny rotation change is a game-changer for hard-core production. But here’s the thing I always tell people: HMCs aren’t for beginners. They’re bigger, heavier, and cost way more upfront. But why do companies shell out that cash? Because of the work envelope. With an HMC, you can fit a rotary table, and that means you can machine all four sides of a part in one setup—no flipping it over, no re-clamping, no risking error when you re-zero the part. For example, if you’re making a engine block, you don’t want to unclamp it halfway because that’s a recipe for alignment issues. HMCs let you do the whole thing in a single go. That’s why big auto manufacturers use them for mass-produced parts, and aerospace shops go to them for complex titanium components that need tight tolerances across multiple faces.
Let’s break down the key differences beyond spindle orientation, stuff that actually impacts your wallet and workflow. First up, chip management. This is a huge one I never skip. VMCs: the chips fall straight down off the part, right into a collection tray under the table. Super easy to clean up. HMCs? The spindle is horizontal, so chips fly every which way. You need a sealed enclosure, a high-powered chip conveyor, and you still have to sweep them out regularly. I see new HMC owners get tripped up here all the time—they don’t account for the extra labor to clear chips, which cuts into their production time. That’s a real cost people don’t calculate at first.
Next, production speed and throughput. Let’s compare apples to apples: same size part, same material. If you’re doing a 50-piece run, VMCs might take a little longer per part, because you have to unclamp, flip, re-clamp, zero, and re-program after each side. But wait—batch size matters. If you’re doing a 1,000-piece run? HMC wins, hands down. No set-up time per side, you can run it lights out for hours while it machines all faces in one go. My buddy has an HMC in his machine shop, he runs it overnight while everyone’s gone, and he cranks out parts way faster than his VMC ever could. But for a 10-piece prototype run? The VMC’s faster because it’s set up and running in 15 minutes, vs an hour to set up the HMC.
Then there’s the footprint and accessibility. VMCs are compact, right? Most of them fit through a standard loading dock door, and you can pull up to the table to load parts without climbing stairs or reaching over a big enclosure. That’s perfect for small shops with limited floor space. HMCs? They’re like a small tank. They need a dedicated spot, a bigger power supply, and a sealed work area so chips don’t go everywhere. Last year, a guy called me wanting to trade his HMC for a VMC because his shop expanded and he had nowhere to put the big guy—VMC’s just way more flexible for tight spaces.
Tolerance and part complexity? Wait, I hear some folks say HMCs have better tolerances, but that’s not exactly right. Modern VMCs can hit ±0.001” just as easily as HMCs for 3-axis jobs. The real win for HMCs is when you need 4 or 5 sides done in one setup, so you eliminate the error from multiple clampings. If you’re doing a simple 2-sided job, a VMC will hold tight tolerances no problem. But if you’ve got a part that needs holes on the top, bottom, left, and right? HMC is the call. I also want to mention spindle power: high-performance VMCs can have 15+ hp spindles that handle most aluminum, steel, even titanium for small parts. HMCs usually have more torque, but that’s overkill for a lot of jobs unless you’re working with really heavy, big parts.
Wait, let’s get real about who should get what. If you’re a new shop, or you mostly do prototypes, small batches, 3-axis jobs, or parts where you don’t need multiple sides? VMC is your go-to. They’re cheaper (a good entry-level 3-axis VMC is like $50k-$80k, vs entry-level HMC is $100k+), easier to operate, less maintenance, and the chip thing is a non-issue. Last month, I helped a startup get their first machine—they make custom medical device implants, small titanium parts for hip replacements, and they only needed 3 sides done, so a VMC was perfect, and they stayed way under their budget. If you’re a mid-sized shop doing consistent high-volume parts, or complex parts that need multiple sides, then HMC makes sense. But I always warn people not to buy an HMC just because it sounds “fancier” if they don’t need the extra capacity. I’ve seen guys drop $150k on an HMC that sits 50% of the time because they don’t have enough work to fill it.
Let me also address some myths I hear all the time. Myth 1: VMCs can’t do high volume. No, they can—just not for extremely large batches, and you have to account for setup time. Myth 2: HMCs are always more accurate. No, like I said, accuracy depends on the machine’s build quality, not spindle orientation. My 10-year-old VMC still holds ±0.0008” for 3-axis jobs, same as my buddy’s 5-year-old entry HMC. Myth 3: VMCs are only for beginners. Nah, I sell high-end 5-axis VMCs to aerospace guys too—they just prefer VMCs for their specific workflow because of the easy access.
So where do I come in here? Like I said, I’m a VMC supplier, and I’m not trying to steer you wrong, but I’ll always be honest: if an HMC is a better fit for your job, I’ll tell you that too. But most of the time, when shop owners come to me asking about the difference, they end up leaving with a VMC because it checks all their boxes—cost, ease of use, flexibility. We build VMCs for every job: 3-axis for small prototypes, 4-axis for rotary parts, high-torque models for aluminum and steel, even 5-axis for complex mold parts. I’ve sold machines to shops that do everything from phone casings to industrial valves, and every time I ask what their main jobs are, I can narrow down if VMC is right for them.
At the end of the day, it’s not about which machine is “better”—it’s about which machine works for your specific work. If you need speed on small batches, easy setup, and don’t have room or budget for a big horizontal machine, VMC is the clear winner. If you’re running 1,000-piece runs of multi-sided parts, and you’ve got the space and cash to back it up, HMC is your guy. But if you’re still on the fence, or you want to run numbers on which will boost your production without breaking the bank, hit me up. I’ve helped hundreds of guys pick the right machine, no sales pitch just real advice. Shoot me a message, let’s chat through your workflow, your part types, and what you’re trying to get done. No pressure, just straight talk.
Engraving and Milling Machine References:
- Machinery’s Handbook, 31st Edition, Industrial Press Inc., 2020
- Modern Machining Technology, 2nd Edition, Goodheart-Willcox, 2018
- National Institute of Standards and Technology (NIST), "Machining Center Capabilities and Limitations," 2021
- SME (Society of Manufacturing Engineers), "Vertical vs Horizontal Machining Centers: A Practical Guide," 2022
Taizhou Qiyang Trading Co., Ltd.
As one of the most professional vertical machining center manufacturers and suppliers in China, we’re featured by quality products and good price. Please rest assured to buy bulk vertical machining center for sale here and get quotation from our factory. Customized orders are welcome.
Address: Zhenhai Village, Binhai Town, Wenling City, Taizhou City, Zhejiang Province
E-mail: qycncmachine@outlook.com
WebSite: https://www.qycncmachine.com/
